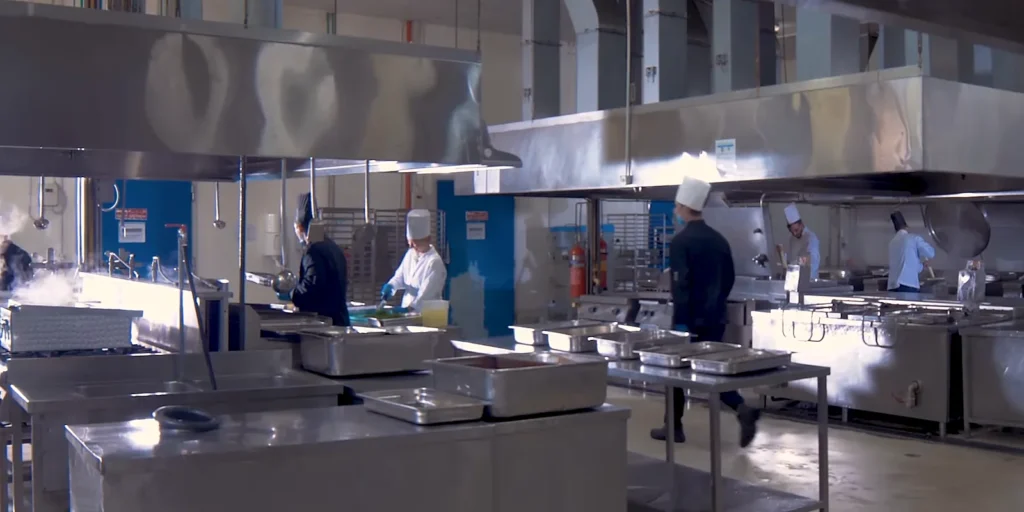
Production at our scale means a lot more than capacity. It means the ability to consistently deliver high volumes without compromising quality, safety or flexibility. Across three facilities, our teams, technology and processes are built to meet demanding specifications across foodservice, retail, healthcare and institutional sectors.
Capacity
At the core of our manufacturing network is a 3,160 m² ready-meals facility, supported by 2 additional vertically integrated production units, specialised facilities for storage and warehousing. This infrastructure allows us to maintain control across key stages of production while adapting efficiently to different products, specifications and market requirements.
45,000+
meals daily
3,160 m²
ready-meals facility
3
facilities, including 2 vertically integrated production units, plus specialised storage and warehousing
Our process
01
Raw Materials
Carefully selected ingredients from approved suppliers, checked for quality and compliance.
02
Preparation
Ingredients are inspected, cleaned, weighed and prepared according to controlled recipes.
03
Cooking & Production
Recipes are prepared under controlled conditions, with quality and food-safety checks throughout.
04
Chilling / Freezing
Products are rapidly chilled or frozen according to their recipe and intended application.
05
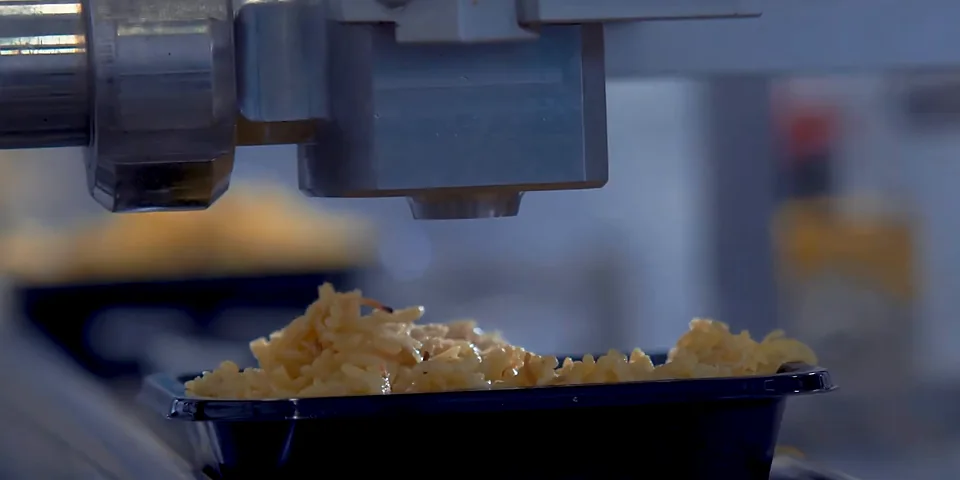
Portioning
Each product is portioned according to defined specifications, ensuring consistency across production.
06
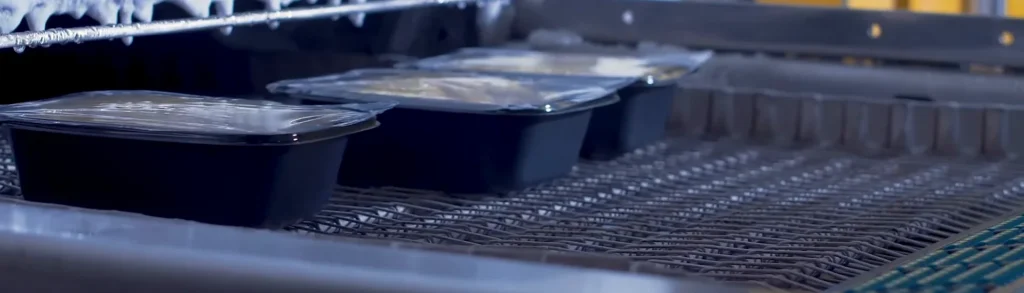
Packaging
Advanced packaging technologies provide secure sealing and protection throughout the product’s journey.
07
Final Quality Check
Products undergo final safety and quality controls before release, including foreign-body detection.
08
Labelling & Traceability
Each pack receives the required product information, coding and traceability data before dispatch.